Hebei Jingye Precision Pipe Manufacturing Co., Ltd.
Tel:+8615373142593
+8618031823787
+8618932936052
WhatsApp: +86 15373142593
E-mail :steeltube@hbjyjt.com
Add: No. 10, Dongzhuang Vilage, Nandian Town, Pingshan County, Shijiazhuang City, Hebei Province
I. Technical StandardsTechnical standards
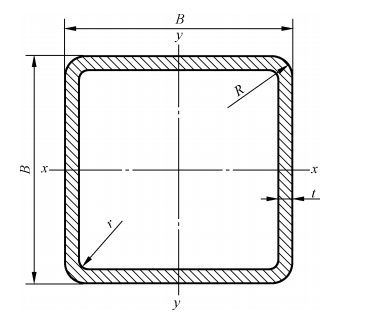
Explanation of indexing symbols:
B -Side length;
t --Wall thickness;
R-Outer arc radius;
r -Inner arc radius;
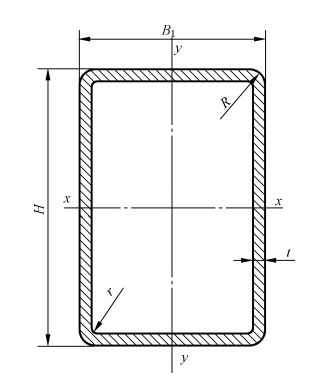
Explanation of indexing symbols:
H - Length of the long side;
B.-Length of the short side;
t - wall thickness;
R -Outer arc radius;
r- Inner arc radius;
(1)Cross-section and allowable deviation
Side length B | Wall thickness | Allowable deviation | |||||||||||||
| mm | 4.5 | 4.75 | 5.5 | 5.75 | 7.5 | 7.75 | 9.5 | 9.75 | 11.5 | 11.75 | 13.5 | 13.75 | 15.5 | 15.75 | (±A,mm) |
| 120 | ±0.90 | ||||||||||||||
| 140 | ±1.10 | ||||||||||||||
| 150 | ±1.20 | ||||||||||||||
| 160 | ±1.20 | ||||||||||||||
| 180 | ±1.40 | ||||||||||||||
| 200 | ±1.60 | ||||||||||||||
| 220 | ±1.80 | ||||||||||||||
| 250 | ±2.00 | ||||||||||||||
| 300 | ±2.10 | ||||||||||||||
| 350 | ±2.80 | ||||||||||||||
| 400 | ±3.20 | ||||||||||||||
Side length mm | Wall thickness | Allowable deviation | ||||||||||||||
| B | H | 4.5 | 4.75 | 5.5 | 5.75 | 7.5 | 7.75 | 9.5 | 9.75 | 11.5 | 11.75 | 13.5 | 13.75 | 15.5 | 15.75 | (±A,mm) |
| 100 | 150 | ±1.20 | ||||||||||||||
| 100 | 180 | ±1.30 | ||||||||||||||
| 100 | 200 | ±1.30 | ||||||||||||||
| 150 | 200 | ±1.50 | ||||||||||||||
| 150 | 250 | ±1.60 | ||||||||||||||
| 150 | 300 | ±1.70 | ||||||||||||||
| 200 | 250 | ±1.60 | ||||||||||||||
| 200 | 300 | ±2.00 | ||||||||||||||
| 200 | 350 | ±2.10 | ||||||||||||||
| 200 | 400 | ±2.40 | ||||||||||||||
| 250 | 300 | ±2.20 | ||||||||||||||
| 250 | 350 | ±2.20 | ||||||||||||||
| 250 | 400 | ±2.60 | ||||||||||||||
| 300 | 400 | ±2.50 | ||||||||||||||
| 300 | 500 | ±3.20 | ||||||||||||||
(2)Length and allowable deviation
1. The usual delivery length of closed-section steel is 4000 mm to 12000 mm. Steel sections of other lengths can be supplied through negotiation between the supplier and the buyer.
2. When closed-section steel is delivered at fixed length or multiple lengths, it shall be specified in the contract. The allowable deviation of its length shall comply with the provisions in the table. If the fixed length accuracy is not specified in the contract, it shall be delivered at ordinary fixed length.
The unit is millimeters | ||
Fixed length precision | Length | Allowable deviation |
Normal fixed length | 4 000~12 000 | +500 |
Precise sizing | 4 000~6 000 | +500 |
>6 000~12 000 | +100 | |
3. Butted delivery of closed-section steel is not allowed. Short lengths and non-fixed lengths not less than 2000mm are allowed for delivery. The weight of short-length and non-fixed-length pipes shall not exceed 5% of the total delivered quantity. For steel sections with a theoretical weight greater than 20kg/m, the weight shall not exceed 10% of the total delivered quantity.
(3)Appearance
1. Determination of bending deviation: The bending degree of the section steel should not exceed 2mm per meter, and the total bending degree should not exceed 0.15% of the total length. The measurement method is shown in the figure.
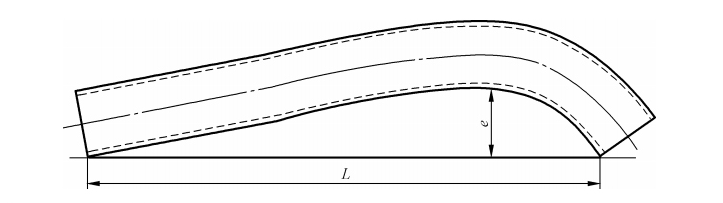
Explanation of indexing symbols:
L一Length;
e- Curvature.
2. Measurement of the torsion degree of square or rectangular section steel: It can be agreed upon by both the supplier and the buyer and specified in the contract to measure the torsion degree of closed cold-formed steel. The measurement shall be carried out on a platform. The measurement method is as shown in the figure, and the measured value shall be less than the V value, which is calculated according to the formula: V = 2 + L × 0.5 / 1000
In the formula:
V-Torsion degree, in millimeters (mm);
L -Length, in millimeters (mm).
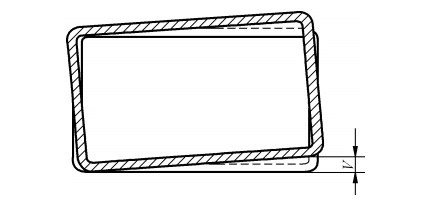
Explanation ofindexing symbols:
V一Degree of torsion.
3. The ends of the section steel shall be cut straight, and the sawing slope shall comply with the provisions in Table 23. Small deformations and burrs caused by the cutting method are allowed.
The unit is millimeters | |
Maximum nominal side length (or nominal outer diameter) | Sawing slope, less than |
≤100 | 2 |
>100~300 | 4 |
>300~500 | 6 |
>500 | Agreement |
4. For open and closed cold-formed steel products that use online thermal cutting processes such as laser cutting or plasma arc cutting, the presence of tiny cutting cracks, nodules, and cutting puncture gaps is allowed. When the total side length of open and closed steel sections exceeds 700mm, more than two cutting puncture gaps are allowed on the same cutting section.
Note 1: Cutting lines refer to the lines left on the cutting surface of the workpiece being cut after the cutting jet blows away the material during the cutting process.
Note 2: Dross refers to the phenomenon where during fusion cutting (such as plasma arc cutting, laser cutting), while the molten metal is blown off at high speed, a portion of it adheres to the lower edge of the cutting surface and solidifies, and this attached substance is called dross.
(4)Weight and Allowable Deviation
Section steel shall be delivered by actual weight. At the request of the buyer, upon negotiation between the buyer and the seller and as specified in the contract, it can also be delivered by theoretical weight.
When delivering by theoretical weight, if the total side length of the section steel does not exceed 1600mm, the allowable deviation between the actual weight and the theoretical weight of each batch of section steel shall be -6% to +10%. If the total side length of the section steel exceeds 1600mm, the allowable deviation between the actual weight and the theoretical weight of each batch of section steel shall be -4% to +6%.
(5)Mechanical Properties
1、The yield strength, tensile strength, and elongation after fracture of section steel shall comply with the provisions in Table 25. The mechanical properties of Q195, Q215, stainless steel or other steel grades shall be determined through negotiation between the supplier and the buyer.
Serial numbe | Product yield strength grade | Upper yield strength ReH/MPa Not less tha | Tensile strength Rm/MPa | Elongation after fracture A/% Not less than |
1 | 235 | 235 | 370~560 | 24 |
2 | 355 | 355 | 470~680 | 20 |
3 | 390 | 390 | 490~700 | 18 |
4 | 420 | 420 | 520~730 | Agreement |
5 | 460 | 460 | 550~770 | Agreement |
6 | 500 | 500 | 610~820 | Agreement |
7 | 550 | 550 | 670~880 | Agreement |
8 | 620 | 620 | 710~940 | Agreement |
9 | 690 | 690 | 770~1000 | Agreement |
10 | 750 | 750 | 750~1010 | Agreement |
For cold-formed steel products with a cross-sectional dimension not greater than 60mm x60mm (including circular and rect-angular cold-formed steels with equal perimeter dimensions) or cold-formed steel products with an edge (shortedge) thick-ness ratio not greater than 14, the percentage elongation after fracture of the flat part is allowed to be 3% (absolute value) lower than the specified value in the table, and the width of the tensile sample used is 12.5mm. | ||||
2. After negotiation between the supplier and the buyer, and as specified in the contract, impact tests can be conducted on cold-formed steel sections with a thickness of not less than 6mm. The results of the impact tests and their re-tests shall comply with the provisions of relevant raw material standards such as GB/T699, GB/T700, GB/T714, GB/T1591, and GB/T4171.
(6)Weld Quality
1. External weld quality
There should be no weld breakage, overlapping welding, burn-through, misalignment, or arc craters at the welds of closed-section steel. Defects at the welds are allowed to be repaired by rewelding and grinding, but after repair, the surface should be flat and smooth, and the thickness after grinding should not be less than the minimum allowable thickness.
2. External burrs of welds
The external burrs at the welded joints of closed-section steel should be removed, and the residual height of the weld after removal should generally not exceed 0.5mm. The internal burrs at the welded joints are usually not removed; if there are special requirements, they shall be determined through negotiation between the supplier and the buyer.
3. Internal Weld Quality
The internal welds of closed-section steel should be continuous, uniform, and full.
4. Other requirements
After negotiation between the supplier and the buyer, and as specified in the contract, requirements for the position of weld seams can be added, including inspecting the mechanical properties and technological properties of the weld seams, as well as conducting non-destructive testing.
II. Disclaimer
1. Unless otherwise guaranteed, the technical information, specifications, etc. contained in this document are all reference values and do not constitute an official guarantee.
2. Customers shall independently confirm the applicability and performance of this product based on the purpose of use, usage conditions, etc.
3. Our company shall not be liable for any damages arising from the use of this product, etc.
Note: Executable standards: GB/T6728-2025, European standard: EN10219, Russian standard: GOST series
Contact Information: +86 15373142593, +86 18031823787, +86 13472220366 (WeChat available)
WhatsApp: +86 15373142593
Address: No. 10, Dongzhuang Village, Nandian Town, Pingshan County, Shijiazhuang, Hebei Province