Hebei Jingye Precision Pipe Manufacturing Co., Ltd.
Tel:+8615373142593
+8618031823787
+8618932936052
WhatsApp: +86 15373142593
E-mail :steeltube@hbjyjt.com
Add: No. 10, Dongzhuang Vilage, Nandian Town, Pingshan County, Shijiazhuang City, Hebei Province
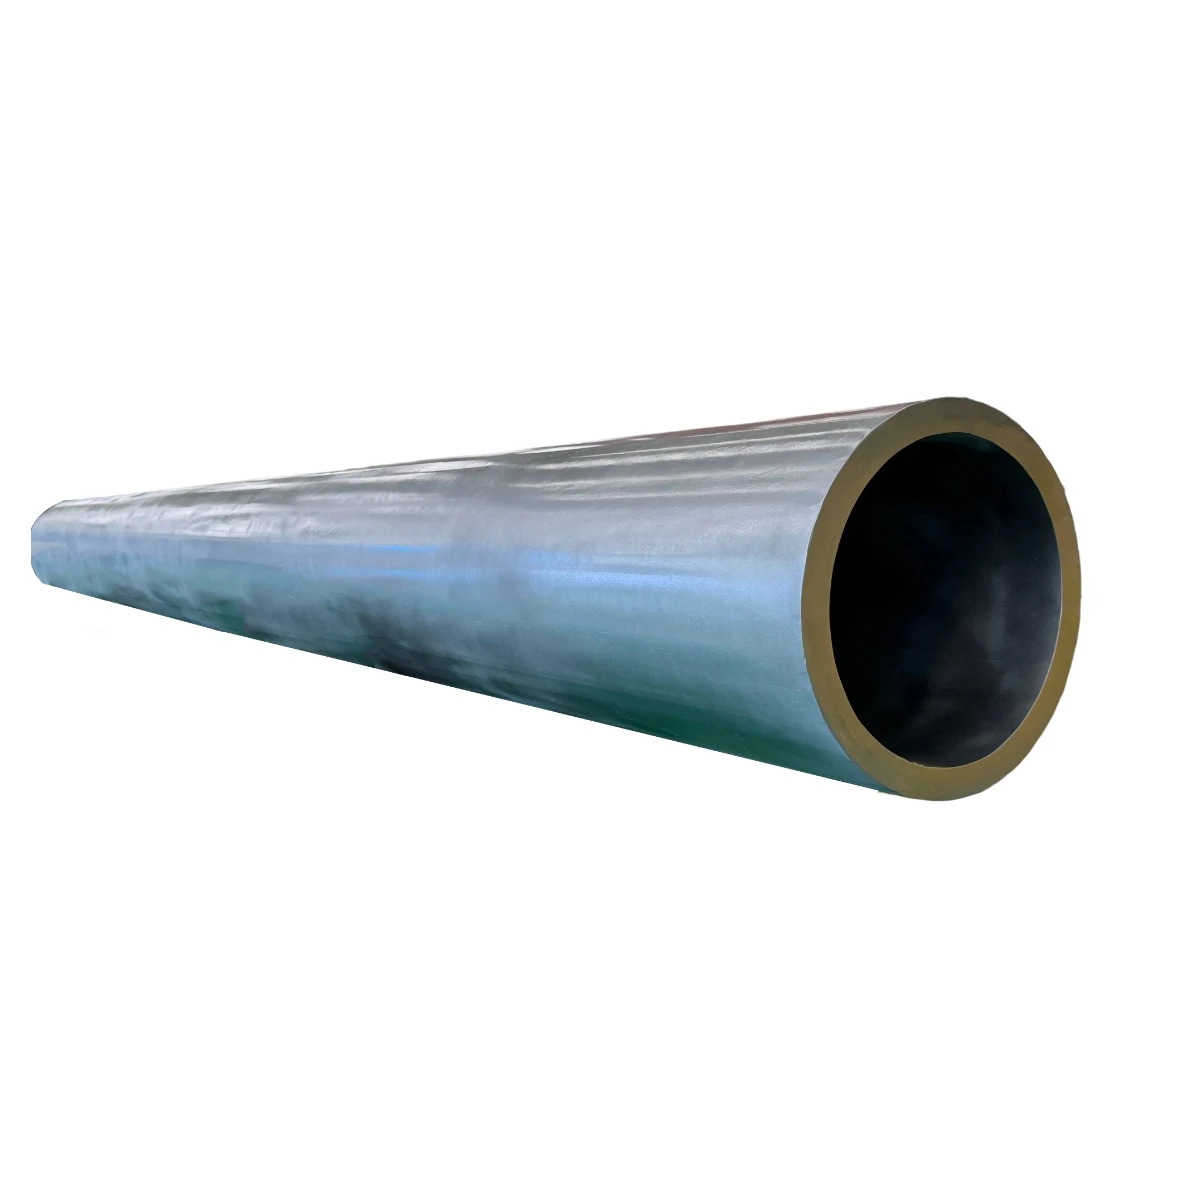
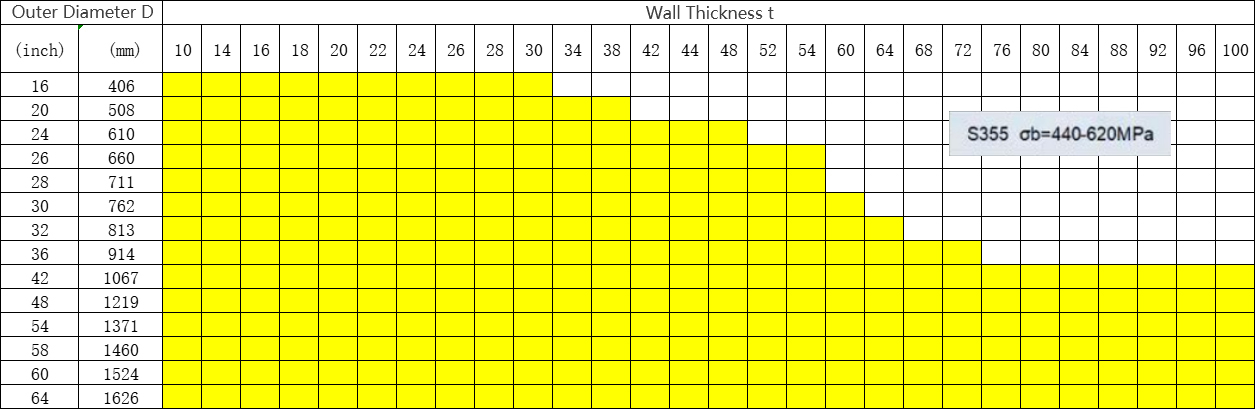
(1) Outer Diameter, Wall Thickness and Allowable Deviation
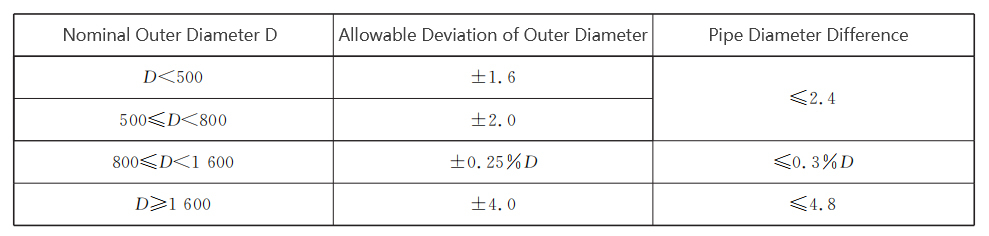
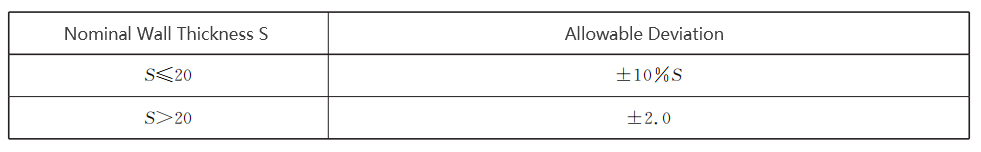
(2) Bending Degree and Out-of-Roundness
1. Curvature: The curvature per meter of the steel pipe shall not exceed 1.5 mm, and the overall curvature shall not exceed 0.1% of the steel pipe length and shall not be more than 10 mm.
2. Out-of-roundness: For steel pipes with an outer diameter to wall thickness ratio not exceeding 75, the out-of-roundness shall not exceed 1.0% and shall not be more than 15 mm. Upon the purchaser's request, steel pipes with other specified out-of-roundness can be supplied after negotiation between the supplier and the purchaser and specified in the contract. For steel pipes with an outer diameter to wall thickness ratio exceeding 75, the out-of-roundness shall be determined through negotiation between the supplier and the purchaser.
(3) Pipe end
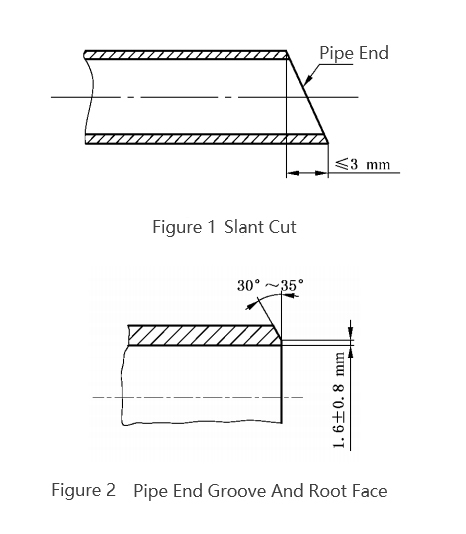
The end face inclination at both ends of the steel pipe shall not exceed 3mm, see Figure 1 for the inclination. Burrs on the cuts shall be removed.
The steel pipes shall be delivered with plain ends. Upon the purchaser's request, through negotiation between the supplier and the purchaser and as specified in the contract, the pipe ends may be beveled. The bevel angle shall be 30° plus tolerance, and the root face shall be 1.6mm with a tolerance of +0.8mm. See Figure 2 for the bevel and root face details.
(4) Weight
1. Steel pipes shall be delivered by theoretical weight. If agreed by both the supplier and the demander and specified in the contract, they may also be delivered by actual weight.
2. The permissible deviation between the actual weight and the theoretical weight of each batch or single steel pipe shall be +10%/-5%.
3. The theoretical weight of steel pipes shall be calculated according to Formula (1).
(1) W =0.0246615(D-S)S
Where:
W -- Theoretical weight per unit length of steel pipe, in kilograms per meter (kg/m), rounded to the nearest 0.01kg/m;
Nominal outer diameter of steel pipe, in millimeters (mm);
Nominal wall thickness of steel pipe, in millimeters (mm).
(5) Mechanical Properties
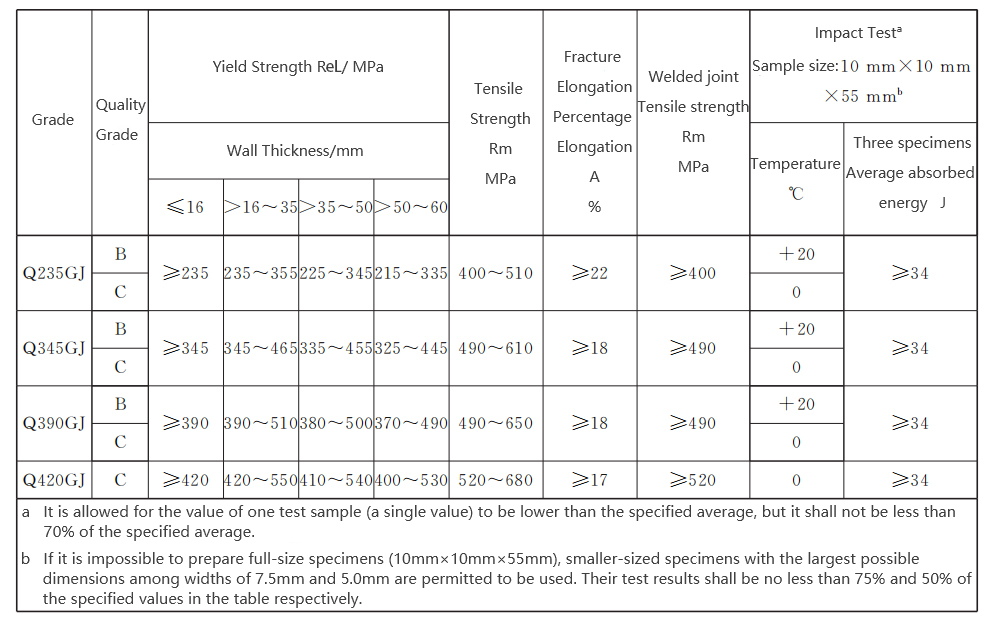
1. Longitudinal tensile test for steel pipes: The longitudinal tensile mechanical properties of the base metal of each grade of steel pipe shall comply with the provisions of Table 1 and Table 2 respectively.
2. Transverse Tensile Test of Steel Pipe: As required by the purchaser, upon negotiation between the supplier and the purchaser and specified in the contract, a transverse tensile test on the base material of the steel pipe may be conducted. The transverse tensile mechanical properties of steel pipes of each grade shall comply with the provisions in Table 1 and Table 2 respectively.
3. Tensile Test of Welded Joints: Steel pipes shall undergo tensile tests on straight seam welded joints. During the tensile test of welded joints, the weld shall be located in the middle of the test piece, and the tensile strength of steel pipes of each grade shall comply with the provisions in Table 1 and Table 2 respectively. At the request of the buyer, through negotiation between the supplier and the buyer and specified in the contract, tensile tests on circumferential welded joints of butt-welded steel pipes may be conducted during welding procedure qualification.
4. Charpy V-notch impact test: Subject to the requirements of the buyer, through negotiation between the supplier and the buyer and specification in the contract,longitudinal Charpy V-notch impact tests on the base metal may be conducted on steel pipes. The impact absorbed energy of steel pipes of each grade shall comply with the provisions in Table 1 and Table 2 respectively.
Table 1 Mechanical Properties of Steel Pipes of Each Grade in GB/T700 and GB/T1591
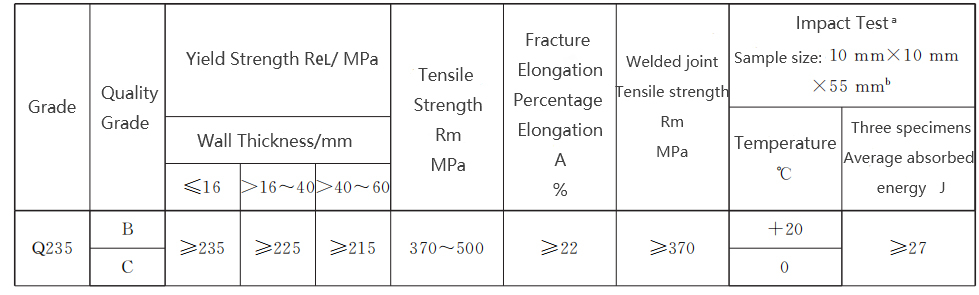
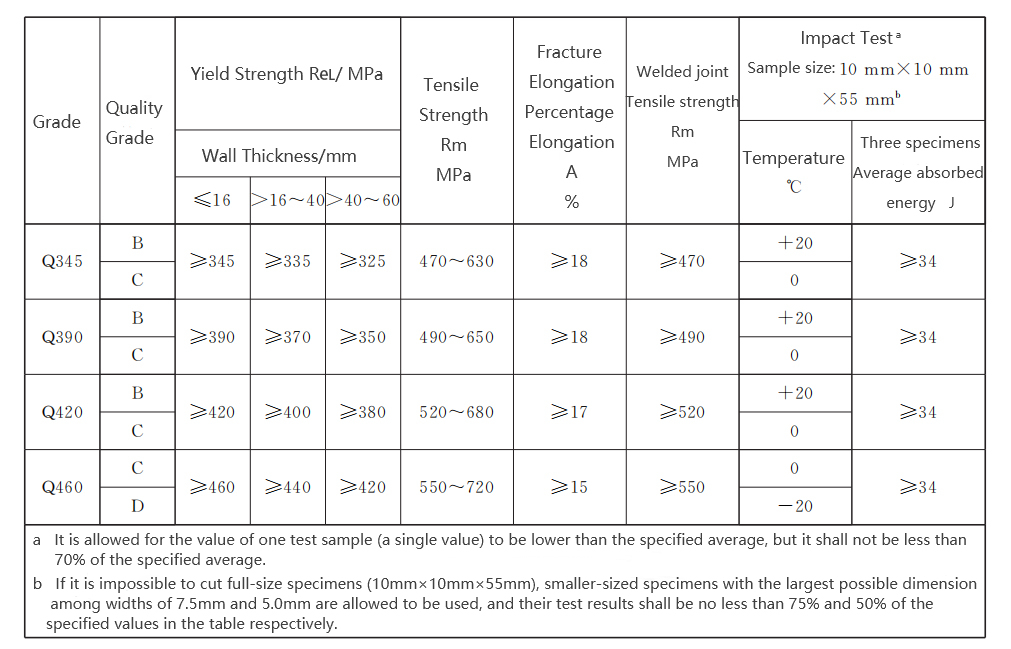
Table 2 Mechanical Properties of Steel Pipes of Each Grade in GB/T19879
(6) Appearance Quality
1. Surface Defects: The inner and outer surfaces of steel pipes shall be smooth. Folds, cracks, shell laminations, weld beads and sharp-bottomed defects (such as scratches) are not allowed to exist. All such defects and sharp-bottomed defects shall be completely removed, and the remaining wall thickness at the defect removal areas shall not be less than the minimum allowable wall thickness. Other local defects that do not exceed the allowable negative deviation of the wall thickness are permitted.
2. Weld reinforcement: When the wall thickness is not more than 12.5 mm, the reinforcement of internal and external welds exceeding the original surface profile of the steel pipe shall not be more than 3.2 mm; when the wall thickness is more than 12.5 mm, the reinforcement of internal and external welds exceeding the original surface profile of the steel pipe shall not be more than 3.5 mm. The excessive part of the weld reinforcement is allowed to be ground and trimmed.
3. Weld Undercut: The weld shall have a smooth transition with the base metal. Undercut with a depth not exceeding 0.5mm may not require grinding treatment.For undercut with a depth exceeding 0.5mm, if the remaining wall thickness after grinding is not less than the minimum wall thickness specified in the design standards, the product can be delivered after grinding treatment; otherwise, repair welding shall be carried out, and the repair welding shall comply with the provisions of 5.10.
4. Radial misalignment: When the wall thickness is not more than 12.5mm, the radial misalignment of the longitudinal seam of the steel pipe shall not exceed 1.5mm; When the wall thickness is more than 12.5mm, the radial misalignment of the longitudinal seam of the steel pipe shall not exceed 12.5% of the wall thickness, with a maximum not exceeding 2.5mm.
(7) Remediation of Defects
For steel pipe weld defects and base material defects with a depth not exceeding 1/3 of the base material thickness, manual low-hydrogen electrode arc welding, automatic submerged arc welding, automatic or semi-automatic metal active gas arc welding may be adopted for welding repair. Before repair, the defects shall be thoroughly cleaned to meet the welding requirements. The weld bead after repair welding shall be ground, and the remaining height after grinding shall be basically flush with the surface of the original steel pipe or the height of the original internal and external welds.
II. Disclaimer
1. Unless otherwise guaranteed, all technical information, specifications and other content contained in this document are reference values only and do not constitute official warranties.
2. Customers shall independently verify the applicability and performance of this product based on the intended purpose and operating conditions.
3. Our company shall not be held liable for any damages arising from the use of this product.
Note: Applicable national standards: GB/T 30063-2013 (Straight Seam Submerged Arc Welded Steel Pipes for Structural Purposes), GB/T 3091-2025 (Welded Steel Pipes for Low-pressure Fluid Transportation); European standards: EN10219, EN 10210; Russian standards: GOST 20295, GOST3262/10704
Contact Information: +86 15373142593, +86 18031823787, +86 13472220366 (WeChat available)
WhatsApp: +86 15373142593
Address: No. 10, Dongzhuang Village, Nandian Town, Pingshan County, Shijiazhuang, Hebei Province